Contents
2. Operation and Control Description
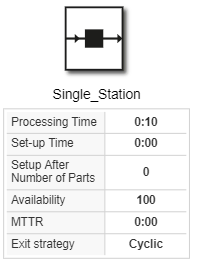
The Single Station object is used to machine parts at a single machining station.
2. Operation and Control Description
The single-station cell receives a single workpiece from its predecessor, processes it, and, once the setup and processing times have elapsed, passes it on in sequence to one of its successors.
If the incoming workpiece types are not identical—that is, if they do not have the same name—the single-station cell must be set up for that workpiece type in order to process it.
While a work order is at the single-station cell, it does not accept any newly arriving work orders but instead adds them to its hold list.
Only after it becomes available again does it accept the held work orders in sequence and process them. If the single-station cell has multiple successors, it transfers the work orders to them in sequence.
If the successor to which the part is to be transferred is blocked—i.e., full or malfunctioning—the individual station does not select another available successor to which it can transfer the part.
Instead, it does not transfer the part and thus becomes blocked.
Only after the successor is free and no longer blocked does it transfer the part and become unblocked. You can also define a different transfer behavior in a method.
Figure 1 - Single Station |
|
© SimPlan AG - Hanau District Court, Commercial Register (Part B) 6845 - info@simplan.de - www.simplan.de/en